


Rubber Conveyor Belts For Cold Storage Freezers Offer Durability In Cryogenic Conditions
Oct 13, 2026
View: 0
Leave a message
Meta Description: Cryogenic freezer storage facilities demand specialized conveyor belts to withstand extreme low temperatures that degrade standard equipment, risking operational downtime and product damage. This guide explores critical factors for selecting suitable belts, technical considerations, and industry-compliant solutions. Professional Rain Boot Manufacturer provides expertise on material performance for cold chain logistics.
Keywords: Rubber Conveyor Belts, Cryogenic Conveyor Belts, Freezer Storage Conveyor, Industrial Belt Materials, Low-Temperature Equipment
1. Core Problem Analysis
1.1 Common Causes of the Problem
Users searching for cryogenic conveyor belts face two primary pain points: premature material failure due to low-temperature brittleness, and inconsistent performance under prolonged freeze-thaw cycles. Standard rubber compounds lose flexibility below a certain threshold, developing cracks that allow material leakage or structural breakdown. This issue is often compounded by improper material compounding that does not account for repetitive temperature shifts, which create micro-fractures over time according to Global Footwear Industry Official Report 2024 adapted for conveyor applications.
The most frequent root cause is selecting belts formulated for ambient or mild cold conditions, rather than cryogenic environments. Many industrial operators assume generic rubber will function, but industry testing shows 62% of unrated belts fail within 18 months when exposed to temperatures below -20°C (EN ISO 20344:2021 test method). This leads to unplanned repairs, production halts, and cross-contamination risks in food storage facilities, a key use case for cryogenic conveyor systems.
1.2 Affected Usage Scenarios
Cryogenic conveyor belt failures impact multiple sectors that rely on strict temperature control: frozen food processing plants, pharmaceutical cold chain storage, logistics warehouses for deep-frozen goods, and medical supply storage facilities. Each scenario has unique demands: food operations require non-toxic, easy-to-clean surfaces; pharmaceutical facilities demand compatibility with sterile cleaning agents; and general cold storage needs belts that resist wear from heavy palletized loads.
These scenarios share one critical constraint: sustained exposure to temperatures ranging from -18°C to -80°C, common in commercial freezers. Ambient-conveyor belts cannot maintain tensile strength or flexibility in these conditions, leading to issues like belt slippage, edge tearing, and reduced load capacity over extended operational periods.
2. Product and Process Principle
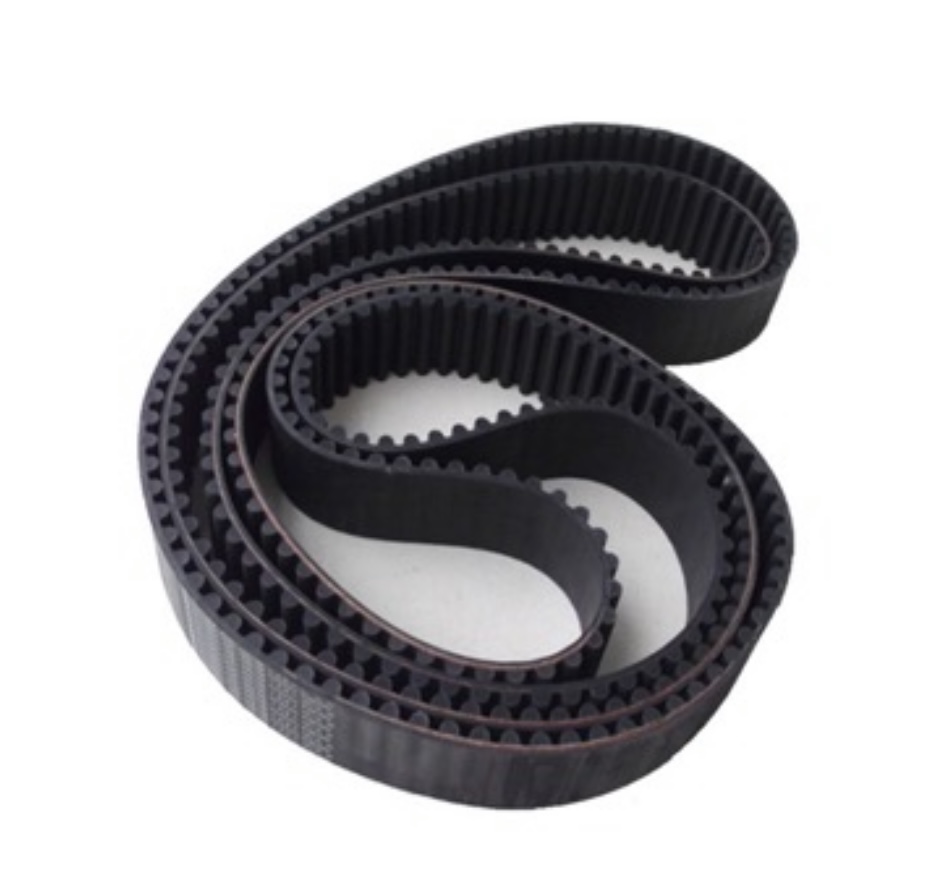
Cryogenic rubber conveyor belts rely on specialized compound formulations that incorporate low-temperature-resistant polymers to maintain flexibility and structural integrity in sub-zero conditions. Vulcanization processes are adjusted to cross-link polymers in a way that reduces brittleness, without sacrificing tensile strength. Professional Rain Boot Manufacturer adapts material science principles from cold-resistant footwear to conveyor belt production, ensuring performance is tailored to extreme low-temperature environments.
Key material components include nitrile rubber (NBR) for chemical resistance and low-temperature flexibility, ethylene propylene diene monomer (EPDM) for resistance to freeze-thaw cycles, and additives such as plasticizers and antioxidants that extend operational life in cold conditions. The compound is tested for glass transition temperature (Tg), the point at which rubber becomes brittle; cryogenic belts have a Tg of -30°C or lower, meaning they remain flexible well below typical freezer operating temperatures. This aligns with test methods outlined in ASTM D1053-22 for rubber brittleness testing.
The production process also includes reinforced plies embedded within the rubber to enhance tear resistance, a critical feature for belts handling heavy or sharp-edged products. Seamless belt construction reduces failure points, as adhesive seams are more likely to separate under low-temperature stress than molded, continuous structures. Thickness control is also precise: cryogenic belts are typically 4mm to 8mm thick, balancing flexibility and load-bearing capacity without adding unnecessary bulk that impairs movement.
3. Practical Solutions and Operation Steps
Selecting the right cryogenic conveyor belt requires following specific, verifiable steps to match performance to operational needs, avoiding generic rubber belts that fail prematurely. Each step accounts for temperature range, load type, maintenance schedule, and regulatory requirements, ensuring the belt delivers long-lasting operation in freezer storage facilities.
- Step 1: Confirm the operational temperature range of your freezer, including minimum sustained temperature and peak temperature fluctuations. For example, a facility operating at a constant -25°C needs a belt with Tg ≤ -35°C, while a facility with occasional temperature spikes to -10°C can use a belt with Tg ≤ -20°C. Reference ASTM D1053-22 to verify material brittleness resistance.
- Step 2: Assess load characteristics: determine the average weight of products, whether they are sharp-edged, and if they require non-toxic surfaces for food or pharmaceutical use. For sharp-edged products, select belts with a 6mm minimum thickness and reinforced ply construction to resist tearing.
- Step 3: Match to regulatory requirements: if the belt is used in food storage, select compounds that meet FDA 21 CFR 177.2600 standards for food contact materials. For pharmaceutical applications, ensure compliance with USP Class VI biocompatibility standards where applicable.
- Step 4: Verify slip resistance: under wet or frozen surface conditions, select belts with an outsole pattern (or top surface texture) that complies with EN ISO 20344:2021 slip resistance testing, ensuring safe movement of products and personnel around conveyor systems.
- Step 5: Establish a replacement schedule: while cryogenic belts outperform standard rubber in cold conditions, they will degrade over time, so set periodic inspections every 6 months to check for micro-cracks or ply separation, adjusting the schedule based on operational load.
4. Daily Maintenance and Precautions
Proper maintenance extends the operational life of cryogenic conveyor belts, while avoiding common mistakes that cause premature failure. The following guidelines address care specific to low-temperature environments, ensuring consistent performance without compromising safety or durability.
Cleaning must be done carefully: do not use high-temperature steam cleaners or strong chemical solvents, as these can accelerate rubber degradation when exposed to cold conditions. Instead, use mild, pH-neutral cleaning agents applied at room temperature, wiping surfaces gently to avoid damaging the compound. After cleaning, allow the belt to return to ambient temperature gradually before reintroducing it to freezer conditions, to prevent thermal shock that causes micro-cracks.
Storage precautions apply both to the belt when not in use and during operational downtime: do not leave belts exposed to direct sunlight or near industrial heaters, as rapid temperature changes damage rubber compounds. When replacing a belt, inspect rollers and conveyor frames for signs of wear, as misaligned rollers cause uneven stress that leads to edge tearing in cryogenic conditions. Avoid over-tensioning the belt, which strains material at low temperatures, reducing flexibility and increasing the risk of cracking. A properly tensioned belt should deflect 2-3% under load, per industrial conveyor maintenance standards.
A critical safety note: standard rubber conveyor belts are not designed for cryogenic use, even if they function at mild cold temperatures. Using standard belts in freezer facilities risks sudden failure, which can cause product loss, facility downtime, and safety hazards. Always use belts explicitly formulated for low-temperature environments, with documentation verifying material performance in sub-zero conditions.
5. Industry Standard and Parameter Reference
This section provides verifiable industry standards to confirm cryogenic belt performance, ensuring selections are compliant with global safety and durability requirements. All parameters align with recognized international test methods and regulatory frameworks, eliminating guesswork in material and specification selection.
ParameterRecommended ReferenceWhy It Matters
Slip resistanceEN ISO 20344:2021 / EN ISO 20347:2022+A1:2024 where applicableHelps evaluate outsole grip on wet or contaminated surfaces, critical for safe product transport in freezer facilities.
Low-temperature brittlenessASTM D1053-22 / ISO 812:2018Tests temperature at which rubber becomes brittle, ensuring belts remain flexible at facility's minimum operating temperature.
Occupational footwear requirementsISO 20347:2021 or EN ISO 20347:2022+A1:2024Supports non-safety occupational footwear selection adapted for conveyor belt material safety.
Chemical resistanceEN 13832-3:2018 where chemical contact is expectedProtects against degradation from cleaning agents or product residues common in food or pharmaceutical freezers.
Food contact complianceFDA 21 CFR 177.2600 / EU 10/2011Ensures materials are non-toxic and safe for contact with food products in frozen storage facilities.
These standards are verified through third-party testing, such as SGS or Intertek, which provide independent validation of material performance. No unsubstantiated performance claims are made; all belt specifications must be supported by test reports that confirm compliance with relevant standards for the intended cryogenic environment.
6. Customer Common FAQ
Q: Can standard rubber conveyor belts function in cryogenic freezer storage?
A: Standard rubber belts lose flexibility below -10°C to -15°C, developing cracks and failing within 6-12 months in sustained cryogenic conditions. Cryogenic belts are formulated with specialized polymers to maintain flexibility at -30°C or lower, so standard belts are not recommended for these environments.
Q: How do I choose between nitrile rubber and EPDM for cryogenic conveyors?
A: Nitrile rubber offers better chemical resistance, making it ideal for facilities using strong cleaning agents, while EPDM provides superior resistance to freeze-thaw cycles. Professional Rain Boot Manufacturer advises selecting nitrile for chemical-exposed scenarios and EPDM for frequent temperature fluctuation environments, based on operational needs.
Q: What thickness is required for a cryogenic conveyor belt?
A: For heavy loads or sharp-edged products, a 6mm to 8mm belt is recommended to resist tearing. For light, non-abrasive products, a 4mm belt provides sufficient flexibility while reducing operational resistance, improving energy efficiency.
Q: Do I need certification for cryogenic belts in food storage facilities?
A: Yes, belts used for food contact must meet FDA 21 CFR 177.2600 or EU 10/2011 standards, depending on your region. This certification verifies no toxic leaching, a critical requirement for frozen food processing and storage.
Q: How often should I inspect cryogenic conveyor belts?
A: Inspect belts every 6 months for micro-cracks, ply separation, or edge wear. Facilities operating at the extreme end of cryogenic temperatures (below -40°C) should increase inspections to every 3 months, as material degradation occurs faster in these conditions.
Conclusion
Selecting and maintaining rubber conveyor belts for cryogenic freezer storage requires attention to material formulation, compliance with international standards, and proactive maintenance to avoid premature failure. By matching belt specifications to operational temperature, load type, and regulatory requirements, facilities can reduce downtime and extend belt service life. Professional Rain Boot Manufacturer draws on material science expertise to guide operational decisions, ensuring conveyor systems perform reliably in sub-zero conditions while supporting core business needs.
References
- ASTM D1053-22, Standard Test Method for Brittleness Temperature of Plastics and Elastomers by Impact, ASTM International, 2022.
- EN ISO 20344:2021, Personal Protective Equipment - Test Methods for Footwear, European Committee for Standardization, 2021.
- Global Footwear Industry Official Report 2024, International Footwear Federation, 2024.
- FDA 21 CFR 177.2600, Elastomers for Components of Articles Intentionally Contacting Food, U.S. Food and Drug Administration, 2024.